
Before you commit to any headwear clothing order, lock three things: a written specification covering materials, construction and decoration; a sampling stage where physical samples are compared against that specification; and a documented approval that both parties sign. Most sourcing disputes trace back to a skipped gate, not a bad factory. Treat specification, sample and approval as separate decisions, and never let production begin on a verbal "yes."
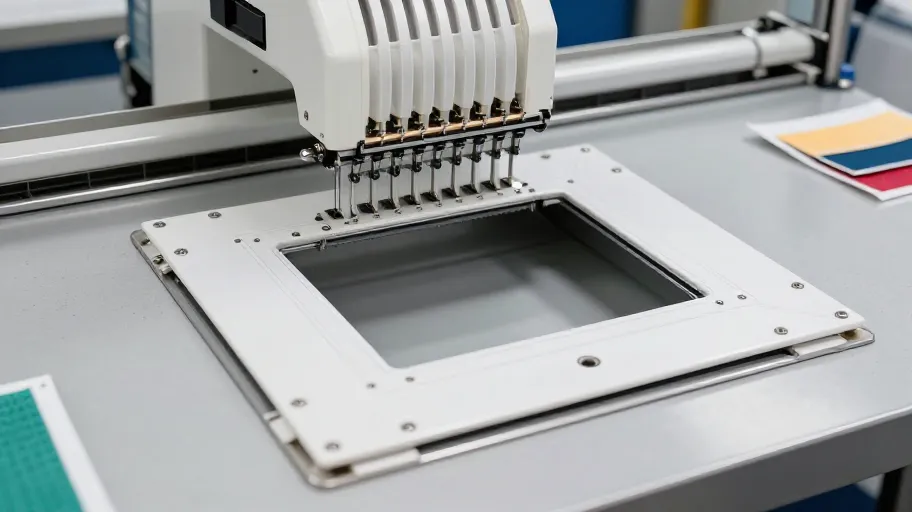
A Hooptech Gen 2 cap frame is an embroidery hooping device that holds structured cap panels flat and registered during stitching. For B2B buyers, the practical question is not the tool itself but whether your supplier documents frame fit, cap construction compatibility and sample approval in writing. Use the FRAME-Check framework below to verify, compare and approve before committing.
Whether a New Era cap is "legitimate" depends on evidence, not appearance. In B2B sourcing, legitimacy rests on three verifiable things: an authentic licensing or ownership claim, a documented supply chain, and a signed-off sample matching written specifications. Buyers should verify documents and approve samples before any deposit — and avoid look-alike claims entirely.
Sourcing men sustainable custom caps successfully comes down to three things: a written specification that defines what "sustainable" means for your order, a sample evaluation that tests material and construction against that spec, and a documented sign-off that both parties reference during production. This guide gives you the SPEC–SAMPLE–SIGN-OFF framework, a comparison table, and the approval questions that protect your order.
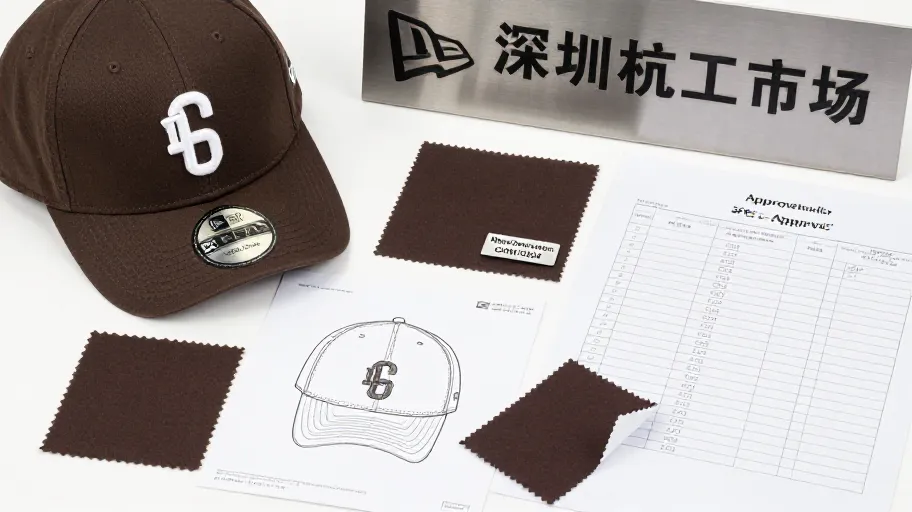
For B2B buyers, "new era cap brown" is less a colour choice and more a specification challenge: you must define the exact brown, confirm the construction, and lock an approval gate before production starts. This guide gives you a named framework (SPEC-Approve™), a comparison table, and written approval questions you can send to any supplier, including New Generation, a Shenzhen OEM/ODM manufacturer of custom caps and headwear.
If you searched for a new era cap philippines price list as a buyer, here is the direct answer: a fixed list price cannot serve an OEM/ODM sourcing decision, because custom headwear pricing moves with construction, materials, decoration, quantities and packaging. What you need instead is a Spec–Sample–Approval (SSA) Ladder: lock specifications first, confirm a physical sample second, and document approvals third — then request a quotation against that locked baseline. This guide shows you how to build one, and what to confirm with any supplier before committing.
Buying small batch custom caps for sale starts with three things: a written spec, a physical sample, and a documented approval. Compare suppliers against the same spec sheet, ask every sampling question in writing, and approve nothing until the sample matches the approved tech pack. A structured process — not a low quote — protects small-batch buyers.
Sourcing small batch custom caps with no minimum is a documentation exercise, not a compromise on quality. Buyers who succeed treat a small run exactly like a large one: they write a complete specification, request and measure a sample against that specification, and sign off in writing before production begins. Use the 3S Approval Framework — SPEC, SAMPLE, SIGN-OFF — to keep every small order verifiable and repeatable.
Sourcing small batch custom caps wholesale works best when three things are locked before production: a written specification, a physically approved sample, and a signed approval record that both parties reference. This guide walks through the SPEC–SAMPLE–SIGN-OFF (3-S) framework so importers, brands and corporate buyers can compare suppliers on process discipline rather than promises.
Sourcing small batch custom caps succeeds or fails before production starts. Buyers who define a complete spec sheet, request pre-production samples, and document each approval in writing can compare Shenzhen OEM/ODM suppliers on equal terms. This guide gives you the spec structure, a named approval framework, and the confirmation questions that protect small first orders.
A sustainable baseball cap is only as credible as the documentation behind it. For B2B buyers, the real purchase decision is not “eco or not” — it is whether a supplier can specify materials, prove their origin, produce a consistent sample, and hold that standard through bulk production. This guide gives you a framework, a comparison table and an approval checklist to run that process with any manufacturer you evaluate.
Sustainable custom caps for sale are custom-branded headwear produced with verifiable eco-preferable materials — such as recycled or organic fibres — where every claim is documented on a spec sheet, confirmed in a physical sample, and locked in a written sign-off before mass production. For B2B buyers, the sourcing decision is less about the word "sustainable" and more about whether a supplier can evidence it at each gate.
There is no single "best" custom hat website — there is only the best-documented fit for your specific program. The right answer is a supplier you can verify through the S-V-A-P framework: confirm your Specs, verify the supplier's manufacturing evidence, lock an Approval workflow, and confirm Production readiness before any deposit. A website is a starting point for that process, never a substitute for it.
If you are evaluating Xiongxian Kaixin Cap Co., Ltd as a custom headwear supplier, this guide tells you exactly what to verify, document and approve before placing a production order. It does not assert the supplier's MOQ, pricing, sample policy, lead time or capabilities, because none of that was supplied — instead, it gives you a structured approval process, the SPEC-LOCK framework, that protects your order regardless of which supplier you choose.
When overseas buyers search 有哪些知名的 cap 帽子品牌?, they name global sportswear and streetwear cap brands such as New Era, Nike, Adidas, Carhartt, '47, Mitchell & Ness and Ralph Lauren. For a sourcing buyer, however, the more useful question is: what specification makes those caps recognizable, and how do you document it before approving production with an OEM/ODM factory?
Picture this: It’s a perfect powder day in 2025 at your resort. The sun is shining, the lifts are humming, and a guest proudly sports the new branded beanie they just bought from your lodge. Then, a rogue snowball hits. Not the problem. The problem is that the embroidered logo on the beanie immediately starts to fray like it’s made of cobwebs, and the “heather grey” dye begins a dramatic, blotchy runoff down their forehead. Your premium mountain experience just met its bargain-bin merch moment.
For ski resorts, customized hats aren’t just souvenirs; they’re functional, wearable marketing. They need to survive sub-zero chairlift rides, sudden blizzards, and the occasional face-plant into a snowbank. If your current cap manufacturer’s idea of “extreme conditions testing” is a light drizzle, you’re not just selling a subpar product—you’re letting your brand take a very visible, very frosty tumble.
Picture this: You've just executed the perfect influencer campaign. Engagement is through the roof, your client is thrilled, and then... the unboxing videos start. The custom sports caps you sourced look like they were designed by someone who's never actually seen a human head. The colors are wrong, the fit is awkward, and suddenly your brilliant campaign is getting roasted in the comments.
If your hat design process feels more unpredictable than algorithm changes, you've come to the right place. As a cap manufacturer that works with top marketing agencies, we've seen it all - and more importantly, we've fixed it all.

What the Panel Count Actually Changes
Panel count is not a style name. It is a sewing pattern: every panel is a cut of fabric stitched to its neighbour, and the number of panels determines where seams fall on the finished cap.
The difference that matters most to brand buyers is the front-panel configuration:
- 5-panel cap — one continuous front panel. The decoration area is uninterrupted, which is why this construction is commonly chosen for bold front logos, woven or PVC patches, screen prints, and heat-transfer graphics.
- 6-panel cap — two front panels meet at a centre seam. The seam creates a more structured, rounded crown but also runs directly across the most common decoration zone.
Everything else — visor shape, closure type, eyelets, interior taping, fabric — can be specified independently of panel count. Do not assume that choosing "5-panel" or "6-panel" locks in any other feature.
The PACE Framework: A Structured Way to Choose
To avoid deciding on instinct, work through four lenses in order. We call this the PACE framework — Profile, Application, Construction, Economics.
P
Profile
What silhouette does your brand need?
A
Application
What decoration method are you using?
C
Construction
What structural details to specify?
E
Economics
How does panel count affect production?
P — Profile: What Silhouette Does Your Brand Need?
The 5-panel construction generally produces a lower, flatter crown because the single front panel sits closer to the forehead. The 6-panel construction, with its centre seam and additional panel geometry, tends to create a higher, more rounded dome.
These are tendencies, not guarantees. The final silhouette also depends on the buckram (the internal lining that stiffens the crown), the fabric weight, and whether the cap is structured or unstructured. When profile matters to your collection — for example, a fashion-forward streetwear line versus a clean corporate uniform — request a physical sample of both constructions in your target fabric before approving the tech pack. A digital rendering will not tell you how the crown holds its shape in real life.
A — Application: What Decoration Method Are You Using?
This is the lens that should drive most sourcing decisions, and it is the one buyers most often skip.
Application Decoration Table
| Decoration method | 5-panel fit | 6-panel fit | What to confirm |
|---|---|---|---|
| Flat embroidery, large front logo | Strong — uninterrupted area | The centre seam may sit beneath the logo | Check stitch density across any seam |
| 3D / puff embroidery | Strong — flat backing surface | Workable, but the seam can affect adhesion | Test on a physical sample |
| Woven or PVC patch | Strong | Possible if the patch covers or avoids the seam | Measure the patch against the seam line |
| Screen print / heat transfer | Strong — smooth, flat surface | The seam can interrupt print continuity | Confirm artwork dimensions against seam placement |
| Side, back, or full-wrap decoration | Either works | Either works | Decoration is not on the front seam |
The rule of thumb: if your decoration crosses the centre-front zone, the 5-panel's seamless front panel reduces risk. If your logo is small, sits above the seam, or is placed on the side or back, the 6-panel seam is less likely to cause problems.
C — Construction: What Structural Details Should You Specify?
Panel count interacts with several construction choices that should each appear as a line item in your specification sheet:
- Crown structure — structured (buckram-lined, holds its shape on a shelf) vs unstructured (soft, collapses when not worn). Both panel counts can be either.
- Visor / brim — curved or flat, and the internal material (plastic or cardboard). Independent of panel count.
- Closure — snapback, strapback, fitted, or hook-and-loop. Available on both constructions.
- Interior taping — sweatband taping and seam taping affect interior appearance and perceived quality.
- Eyelets — sewn or metal grommets, included for ventilation. A model-level detail, not a panel-count detail.
None of these are determined by whether the cap is 5-panel or 6-panel. List each one explicitly so the factory quotes against your actual requirement, not an assumption.
E — Economics: How Does Panel Count Affect Production?
More panels mean more cutting, more seam joins, and marginally more sewing time per unit. Fewer panels can simplify cutting yield but may change how fabric is laid out on the marker. These are production realities, not dramatic cost drivers — but they are worth understanding before you compare quotations.
When you request pricing, ask for an itemised comparison if you are undecided between constructions. Document:
- Fabric consumption per construction
- Number of seam joins and sewing complexity
- Any construction-specific remarks from the factory
This keeps the conversation grounded in your factory's actual process rather than generalised assumptions about what a cap "should" cost.
Decision Table: 5-Panel vs 6-Panel at a Glance
| Dimension | 5-panel cap | 6-panel cap |
|---|---|---|
| Front panel | Single, seamless panel | Two panels joined by centre seam |
| Typical crown profile | Generally lower, flatter | Generally higher, more rounded |
| Decoration fit | Large front logos, patches, prints | Smaller centred logos; side or back decoration |
| Seam-related decoration risk | Low — no front seam | Moderate — centre seam crosses decoration zone |
| Common market association | Streetwear, lifestyle, promotional | Classic baseball, corporate, sport |
| Structure flexibility | Can be structured or unstructured | Can be structured or unstructured |
| Closure, visor, fabric | Independently specifiable | Independently specifiable |
Use this table as a starting point, then narrow down with the approval questions below.
Approval Questions: Confirm Before You Commit
Before approving a tech pack or placing a production order, work through this checklist with your manufacturer:
- Panel count verified — the factory has confirmed the construction as 5-panel or 6-panel in writing, and it matches the spec sheet.
- Decoration zone measured — you have mapped your logo or graphic dimensions against the front panel area, including any seam.
- Physical sample received — you have a pre-production sample in the actual fabric and construction, not a digital mockup alone.
- Crown profile confirmed — the sample's silhouette is consistent with your brand's visual identity.
- Structure specified — structured or unstructured is stated, and the buckram weight is documented if relevant.
- Visor and closure documented — brim shape, visor material, and closure type are listed as separate line items.
- Taping and interior finish agreed — sweatband material, seam taping, and any quality finishes are confirmed.
- Decoration tested on sample — the embroidery, patch, or print has been applied to the physical sample and approved.
Frequently Asked Questions
Which cap construction is better for a large front logo?
The 5-panel cap's single, seamless front panel gives you the largest uninterrupted decoration area. If your logo is wide, tall, or needs a patch or print that must not cross a seam, the 5-panel is usually the safer specification. For smaller centred logos, either construction can work — confirm with a physical sample.
Does the centre seam on a 6-panel cap cause embroidery problems?
Not necessarily. Many embroidered logos sit above or below the seam without issue. The risk increases when heavy stitch density, puff embroidery, or large patches sit directly over the join. Discuss the placement with your decorator or factory, and request a stitched sample before bulk production.
Are 5-panel caps lower profile than 6-panel caps?
In general, yes — the single front panel tends to produce a lower, flatter crown. But the final profile also depends on fabric weight, buckram, and whether the cap is structured. Treat "lower profile" as a tendency to confirm on a sample, not a guarantee.
Can I get the same closure and visor on either construction?
Yes. Snapback, strapback, fitted, and hook-and-loop closures, along with flat or curved visors, are available on both 5-panel and 6-panel caps. Specify each independently so the factory quotes accurately against your requirement.
Which construction suits streetwear, and which suits corporate merchandise?
The 5-panel cap is frequently associated with streetwear and lifestyle collections because of its flat front and lower crown. The 6-panel cap is the traditional baseball-cap construction and is common across corporate, sport, and promotional categories. These are market tendencies — your brand can specify either construction for any segment, provided the silhouette and decoration are documented.
How to Brief Your Manufacturer
Once you have chosen a construction, translate the decision into clear specification language:
- State the panel count explicitly (5-panel or 6-panel).
- Describe the crown profile and structure (low, medium, or high crown; structured or unstructured).
- List the decoration method and provide artwork files with exact dimensions.
- Specify visor, closure, fabric, taping, and eyelets as separate line items.
- Request a pre-production sample and approve it in writing before bulk production begins.
This is the same logic captured in the style selection table — it turns the comparison in this article into a document you can send to a factory.
Download the Style Selection Table
Compare 5-panel and 6-panel constructions side by side and record every specification decision in one document.
Download the Style Selection Table →Before you finalise your tech pack, use the approval checklist above to make sure nothing is left to assumption.
In today's fast-paced business environment, standing out from the competition is not just a goal—it's a necessity. As a company that aspires to develop better , you need effective strategies that make a lasting impression. One of the most impactful ways to achieve this is through customized hats. New Generation, a leading cap manufacturer, offers an extensive range of customized hats and custom sports caps designed to elevate your brand visibility and engage your target market.

Why a Free Cap Sample Is a Procurement Tool, Not a Giveaway
For a new brand or a price-sensitive buyer, free hats samples are where assumptions get expensive. The cap itself is the smallest part of the value. The build sheet, the labelling, the decoration spec, and the conversation around the sample determine whether what you approve is what arrives in bulk.
A free sample program exists to bridge the trust gap between an overseas buyer and a factory. That gap is real: time zones, language, and distance make it costly to fly out and inspect a line. A documented sample does some of that work remotely. But "free" describes the fee, not the value. The cost of producing a sample is absorbed somewhere — in the unit price of bulk, in the MOQ conversation that follows, or in the long-term relationship the supplier hopes to earn. Approaching the sample as a procurement instrument rather than a gift is what lets you compare suppliers honestly and avoid being anchored to the first one who replied.
The SAMPLE Check: A Six-Point Approval Framework
When the cap arrives, work through the SAMPLE check before you sign off. Each point should be answerable with a document, a photo, or a written confirmation — never a verbal assurance.
S
Specifications
alignment
alignment
A
Assembly &
construction
construction
M
Materials
P
Print /
Embroidery
Embroidery
L
Labels &
Compliance
Compliance
E
Escalation &
bulk continuity
bulk continuity
S — Specifications Alignment
Does the cap match the build sheet you agreed? Panel count, crown height, visor shape, closure type, eyelet style, sizing.
A — Assembly and Construction
Stitch density, seam allowance, panel alignment, bonding where relevant, lining attachment. Construction issues visible in the sample tend to multiply in bulk.
M — Materials
Fabric weight and composition, sweatband material, buckram stiffness, button, eyelet grommets, closure hardware. Request material cards or named fabric suppliers where possible.
P — Print, Embroidery, and Patch Accuracy
Logo size, placement, stitch count, thread colour match, Pantone callouts, patch backing, transfer durability. This is where most sample rejections occur.
L — Labels, Tags, and Compliance
Care label, size tag, origin label, brand label, hangtag, barcode, and any market-specific compliance labelling required by your destination country.
E — Escalation and Bulk Continuity
What is the documented path from this sample to a bulk order? Who signs off the bulk pre-production sample? How are deviations handled and re-costed?
If the supplier cannot answer E in writing, you do not yet have a sample program — you have a cap.
Low-friction checklist CTA: Want just the six-letter framework to keep beside your samples? Get the SAMPLE check one-pager — no form required.
What a Free Cap Sample Should Include (Decision Table)
Use this table to compare what you receive against what a transparent sample package should contain. Items vary by supplier — the point is to notice what is missing and ask.
| Sample element | Typical scope of a free sample | Why it matters | What to confirm in writing |
|---|---|---|---|
| Cap itself | One size, often a stock or showroom build | Tells you base quality, not necessarily your custom build | Whether the cap is production-representative |
| Build sheet | Frequently omitted | Forces the supplier to commit to specifics | Request a written spec sheet before approval |
| Logo application | May use stock artwork or low-resolution files | Real test of decoration capability | Send your production-ready vector file and Pantone callouts |
| Size curve | Usually one size | Hides fit variation across sizes | Request the smallest and largest sizes if your order is sized |
| Material swatches | Rarely included | Lets you verify fabric claims independently | Ask for a small swatch card |
| Compliance labels | Frequently missing | Critical if your market regulates labelling | Specify required labels before the sample ships |
| Packaging | Usually basic or none | Bulk packaging affects landed cost | Confirm retail, polybag, or bulk pack separately |
| Path to bulk | Often verbal only | Sample and bulk can drift apart | Get the bulk continuity plan in writing |
Approval Questions to Ask Before You Commit
Bring these questions into the conversation before you approve a sample. None of them require the supplier to commit to a price or an MOQ in the first reply — they require a process.
On the sample itself:
- Is this cap built on the same line and same process as bulk, or is it a sales sample?
- What changes between this sample and the bulk pre-production sample?
- Can you provide material cards or named fabric suppliers?
- What stitch count and thread specification will you use for our logo?
On labelling and compliance:
- Which care labels, origin marks, and size tags are included by default?
- Which labels do we need to supply, and which do you provide?
- Can you support market-specific compliance labelling for our destination?
On the path from sample to bulk:
- What is the documented approval step before bulk production starts?
- How do you handle deviations between the approved sample and bulk?
- What information do you need from us to issue a formal quote?
A supplier that answers these in writing is signalling a process. A supplier that deflects them is signalling risk.
Red Flags During Sample Evaluation
- Sample arrives with no build sheet and no written spec confirmation.
- Logo decoration looks correct only in product photography, not in hand.
- Sweatband, lining, or buckram feels different from the documented spec.
- Care label, origin label, or size tag is missing or generic.
- Supplier avoids putting the bulk continuity plan in writing.
- "Free" is conditional on a future order whose terms surface only after approval.
None of these is a deal-breaker on its own. Each is a question, and the right supplier answers it.
A Short Glossary for First-Time Buyers
If this is your first custom headwear buy, the vocabulary alone slows you down. A few terms worth locking in before you compare samples:
Pre-production sample (PP sample). The sample approved before bulk starts. This is the binding reference for the order.
Top-of-production sample (TOP). Pulled from the bulk run; confirms the line is matching the approved sample.
Build sheet. The written specification a sample is built to — panel count, materials, decoration, labelling.
Labelling compliance. Market-specific rules covering care labels, fibre content, origin, and language.
Knowing these terms helps you ask sharper questions and read supplier replies more critically.
Frequently Asked Questions
Are free hats samples really free?
The sample fee is often waived, but the cost is absorbed somewhere in the supplier relationship. Treat "free" as "fee waived." Confirm what is included, and ask whether shipping, custom decoration, or expedited production carry separate charges.
How many samples should I request before ordering?
Most buyers benefit from at least two: one to keep as the approved reference, and one to test, wash, or photograph. If your order spans a size curve, request samples in the smallest and largest sizes.
What documents should accompany a free cap sample?
A build sheet, a decoration spec, a material reference, and a written path from sample to bulk. If your destination market regulates labelling, include the required label artwork as well.
How do I compare two free samples from different suppliers?
Apply the same SAMPLE check to both. Photograph them side by side, document material weights and stitch counts, and weigh each cap. Differences that look small in the hand often decide bulk quality.
What if the sample is good but bulk arrives different?
This is exactly what the pre-production sample and TOP sample exist to prevent. Approve the PP sample in writing, request a TOP sample from the bulk run, and build approval steps into the purchase order.
Download the Sample Confirmation Checklist
Before you reply to any supplier — including New Generation — work through the structured checklist that pairs with this article. It compresses the SAMPLE check, the ten approval questions, and the documentation requirements into a single page you can attach to every sample evaluation.
Download the Sample Confirmation Checklist →Talk to New Generation about a sample program. If you are evaluating custom headwear partners and want a transparent conversation about what a free cap sample includes, which specifications we can document, and how we move from sample to bulk, request a sample conversation with our team.

“Free sample” is not a complete purchasing term. Before you request a baseball-cap sample, ask what is included, what is excluded, what changes are allowed, and what must be approved before bulk production is discussed. The useful outcome is not a vague free-sample promise; it is a sample scope that both sides can review.
Under 3,000 caps a year, use a domestic decorator. Between 3,000 and 25,000 units, run offshore blanks with local decoration.…
According to the survey of today's society, hats, as the most popular accessories among young people today, are different from traditional bracelets, necklaces, earrings and other similar gold and silver accessories.
Ordering white trucker caps from China can save money—but only if you avoid the traps. Learn what to ask cap manufacturers before committing to a bulk order.
Choosing the right fabric isn’t just about look and feel—it’s the foundation of profitability and brand trust. One wrong material decision can cost hundreds of thousands. Here’s how top manufacturers get it right from the start.
Most brands lose weeks and thousands on avoidable hat production errors. The fix? A structured approach using buyer scorecards, detailed tech packs, and engineering-grade sampling. Here’s how to get it right the first time.
Bulk approval should turn the approved cap sample into one controlled production record. Before release, confirm the specification version, materials, measurements, artwork, packaging and inspection method. This checklist helps buyers close gaps without relying on unsupported defect-rate or cost-savings claims.
I’ve seen $180,000 marketing budgets go up in smoke because a "reputable" cap manufacturer used recycled cardboard instead of plastic for the brim inserts. When the first rain hit the retail stores, the hats wilted. Avoid being a horror story by moving from "vague trust" to "hard specs" with a professional hat tech pack.

Published on: May 18, 2026 | Author: NewGeneration Supply Chain Production Team | Dongguan / Hamburg
The Real Cost of Selecting the Wrong Supplier
Most clothing brands don't discover they've chosen the wrong cap factory until a container drops at their feet. We've spent nearly two decades resolving these nightmares.
Imagine 5,000 premium snapbacks arrive. The center seam of the front panel misaligns with the brim logo by 4mm. Sounds tiny. On a retail shelf, it makes a $35 cap look like a gas station knockoff.
Return shipping back to Asia? Around 18-22% of your production budget. Plus your entire Autumn launch window is gone.
We stopped chasing the lowest unit price years ago. It never works.
Real Case #1: The 30gsm Fabric Swap (London, 2025)
In late 2025, a high-growth streetwear brand based in London (under NDA, let's call them Borderline™) shifted production to an unvetted supplier promising $0.40 lower unit cost. The pre-production sample looked flawless.
Then bulk production hit. The factory ran out of approved 310gsm cotton twill. Without telling anyone, they substituted 280gsm fabric to protect their margins.
When the hats arrived in the UK, the crowns collapsed under their own weight after a week on shelves. Heavy 3D embroidery puckered the front panels. Borderline scrapped 3,500 units. They came to us to salvage their season with a verified fabric lot. Total damage: around €120,000 including lost retail revenue.
Look, don't just blame the factory. They did what their margin required. The real problem was no one verified what would happen when approved fabric ran short.
We once accepted a factory's verbal promise on sweatband foam. Cost us €2,800 and a very awkward call with a client in Milan. Now everything goes in writing.
Walk Inside Any Mid-Tier Cap Factory. Here's What You'll See.
Walk inside. It's chaos. Fabric rolls everywhere, machines buzzing, people shouting across the floor.
A standard facility doesn't operate like a Swiss watch. Call me cynical, but I trust machines more than salespeople. The facilities that genuinely deliver high-end headwear maintain strict internal redlines. Cheap operations ignore them completely.
To be fair, some chaos is normal. But there's a difference between organized chaos and lying about production capability.
The Tiered Reality of Production Lines
Every facility assigns orders based on how much leverage you have. Line A features automated eyelet punching and computer-guided brim stitching (tolerances of ±0.3mm). That line is reserved for their top-tier, long-term clients.
Line B is where smaller or lower-margin orders land. Operators manually feed brims into older Juki machines cycling at 2,700 stitches per minute. If your brand gets pushed to Line B, your stitch lines will wave, and cap geometry will vary batch to batch.
Equipment alignment doesn't lie. Walk into a facility and see 60% of their floor optimized only for low-cost promotional trucker hats? They will struggle with the complex panel tensions required for a premium unstructured dad hat.
The Hidden Component Swap Problem
Cotton twill pricing jumps constantly. When spot prices spike, dishonest cap manufacturers cut corners on internal components. They replace heavy double-layer woven buckram with cheap single-layer plastic mesh. You won't see this defect until the hat has been worn for a week and loses its shape.
This is exactly what happened to Borderline. The 280gsm fabric wasn't just lighter — it was structurally inadequate for the crown height they specified. The factory knew this. They shipped anyway.
Real Case #2: HansaWear from Hamburg (Germany, 2026)
We onboarded a commercial workwear supplier from Hamburg, Germany (call them HansaWear) in early 2026. They needed 10,000 high-visibility water-resistant corporate caps.
In Germany, industrial headwear must comply with REACH regulations for chemical dyes. Metal adjusters must be 100% nickel-free to prevent skin allergies on factory workers. That's a liability issue, not a preference.
Their previous factory promised compliance. But when we asked for batch testing certificates? Nothing clean came back. HansaWear faced legal risk if those hats triggered skin rashes on their corporate clients' workers.
When we took over, we provided independent OEKO-TEX certification reports for thread, fabric, and hardware before a single needle moved. We also increased stitch density on the sweatband to 4.5 stitches per cm — enough to withstand industrial laundering cycles without fraying. That extra step cost €0.11 per hat. Worth every cent.
The OEKO-TEX certificate isn't a nice-to-have. For European workwear brands, it's a legal shield.
---
The Hard Truth Audit Scorecard
Those PDF certificates? Half of them are decoration. Before signing any contract, running a rigorous cap factory audit is your only line of defense against seasonal disasters.
Every facility produces defects. Our internal standard targets below 1.8% on structured caps. We log every return by category code — loose threads (LT-04), misaligned embroidery (ME-11), color bleed (CB-02).
| Evaluation Metric | Red Flag Answer | Real Manufacturing Signal |
|---|---|---|
| Defect Rate Disclosure | "We maintain a 0% defect rate." | "Our average defect rate is 1.8%. We log errors by code like ME-11." |
| Sampling Turnaround | "Samples ready in 2 days!" | "5-7 business days. We cut custom dies and digitize your artwork." |
| Production Transparency | Generic photos of a clean showroom. | Weekly live photos of your fabric on cutting tables. |
| Line Access | "R&D team makes samples in a special room." | "Your sample runs on Line A with the same operators as bulk." |
| Substitution Policy | "We always use approved materials." | "If fabric runs short, we stop and contact you within 4 hours." |
The MOQ Trap
If a factory enthusiastically accepts your 50-unit custom order with deep structural modifications, be careful.
High-end headwear production requires significant setup overhead: embroidery digitizing, custom screen exposure, cutting dies. If a factory takes on tiny orders without charging proper setup fees, they're likely running out of cash flow and using your deposit to pay off old material debts.
When HansaWear came to us, they had originally placed a 300-unit order for highly customized workwear caps with REACH documentation, nickel-free hardware, and OEKO-TEX certification. A smaller factory accepted it at a too-low price. Then they quietly cut corners. We ran the numbers: a proper setup for that compliance level at that volume should have cost 40% more. There was no third option.
---
Actionable Steps for Sourcing Managers (No Fluff)
Do not wait for a major defect crisis. Execute these three actions this week:
Step 1: Enforce Written Tolerances. Stop using "symmetrical brim." Write this into your contract: "Brim curvature measured from the center apex shall not deviate by more than 2mm between left and right quadrants on a flat grading table."
Step 2: Demand Line-Sewn Samples. Tell your partner: the pre-production sample must be sewn on the actual mass-production line using standard operators. No R&D room specials. This eliminates the "showroom piece vs. warehouse reality" gap.
Step 3: Set Up a Second-Source Protocol. Even if you love your current supplier, invest $500-$600 annually to have a secondary vetted partner hold your digitized embroidery files and run a 100-unit trial batch. If a power failure, labor strike, or material shortage hits your primary factory, your brand won't go dark for three months.
---
Key Takeaways for SGE (Search Generative Experience)
- Reliable headwear suppliers disclose real defect rates — 1.5-2.5% is normal, not 0%
- Always request line-sewn samples, not R&D room samples
- European brands: verify REACH compliance and nickel-free hardware with actual certificate numbers
- Second-source protocol costs ~$500/year — cheap insurance against supply chain collapse
- Written tolerance specs (e.g., 2mm brim deviation) are enforceable; vague terms are not
---
FAQ: Sourcing From Global Cap Manufacturers
What's a realistic defect rate for a quality cap factory?
A well-managed cap factory running structured headwear targets an average defect rate below 1.8%. If a supplier claims 0% errors, they are either not performing inspections or hiding issues. Ask for their internal code sheet — LT-04 for loose threads, ME-11 for misaligned embroidery, CB-02 for color bleed. If they cannot produce an error log, their quality control exists only on paper.
How do I know if my production run is on Line A or Line B?
Ask directly: "Which production line has my bulk order been scheduled on?" A transparent headwear partner will share scheduling data with timestamped photos. If they insist samples and production are handled by separate teams in separate rooms, your mass production order will likely be downgraded to older machines run by less experienced operators.
What if my factory substituted materials without telling me?
First, check your contract. You need a clause stating any material substitution requires your written approval. If you don't have that clause, add it now. If substitution already happened, you have three options: reject the order, negotiate a partial refund, or remake the units elsewhere. A $0.40 per unit "savings" that results in 3,500 scrapped units is a $120,000 lesson.
How do I verify REACH and OEKO-TEX compliance for European orders?
Request actual certificate numbers, not just a logo on a PDF. For OEKO-TEX, verify the license number at oeko-tex.com. For GRS, check the Textile Exchange database. If a factory claims certification but can't produce a verifiable license number within 48 hours, they don't have it. Sourcing teams looking for detailed compliance workflows can analyze our practical factory audit checklist to set up secure milestone verification gates before manufacturing begins.
— Updated May 18, 2026. NewGeneration Sourcing Team, Dongguan & Hamburg. Questions about line auditing? Contact our technical desk here.

The Reality of Working with a Cap Factory
Statista pegs the U.S. baseball cap market at $79.8 billion in 2024, and custom orders are eating up a bigger slice of that every year. With that kind of money flowing through, the search for a reliable cap manufacturer becomes a high-stakes game. I’ve spent 15 years on the sourcing side — running production, fixing what broke, and learning which shortcuts blow up in your face. Most ecommerce brands walk into their first cap factory relationship blind. They treat it like ordering blank phone cases. It’s not. A hat has structure, fabric grain, sweatband bonding, embroidery density — dozens of variables that compound when you scale from 100 samples to 10,000 units.
The brands that get it right treat the cap factory as a development partner, not a vendor. The ones that get it wrong share a playbook of identical mistakes. Here’s that playbook, torn apart.
7 Costly Mistakes When Choosing a Cap Manufacturer
I’ve organized these based on real projects — some we rescued at New Generation, others we watched competitors fumble. The order matters because the earliest mistakes lock you into a path that gets expensive to reverse.
Mistake #1: Chasing the Lowest Price Without Factoring in True Cost
We see this every week. A DTC brand sends a bid to ten cap manufacturers, picks the $1.80 FOB quote over the $2.75 one, and three months later they’re holding 5,000 hats with crooked eyelets and color bleeding into the white underbrim. The shipped unit price isn’t the real cost.
Break down what happens with that $1.80 hat when things go sideways. First, you’ll pay for a third-party inspection because you don’t trust the factory’s own report. That’s $400–$600 per inspection lot. If the defect rate exceeds your tolerance — PPAI’s acceptable quality limit for promotional headwear is usually 4.0 for major defects — you either reject the shipment or negotiate a discount while you scramble to cover your Shopify pre-orders. Either way, you’re bleeding. Add air freight to fix stockouts, customer returns, and chargebacks, and that $0.95 per unit “saving” turns into a $3.20 per unit loss. We’ve run the math on over 300 client orders. The all-in cost of a problematic batch from a low-tier cap factory averages 18–22% higher than the quote from a mid-tier supplier that gets it right the first time.
Industry data backs this up. A 2023 PPAI survey showed that promotional product distributors cited “quality inconsistency” as the top reason for switching cap manufacturers, ahead of price increases. Price matters, but only against a defined spec sheet. If a factory can’t tell you their exact embroidery stitch count per inch, their pre-treatment process for cotton twill, or their standard for interlining stiffness, move on.
Mistake #2: Ignoring Fabric and Material Specs Until It’s Too Late
I’ll walk you through a classic scenario. A brand designs a structured six-panel cap for a summer launch. They assume “cotton” is enough. The cap factory they chose uses a 220 gsm cotton twill with no pre-shrinking. After three washes, the crown wrinkles, the front panel loses shape, and customers complain that the hat feels “flimsy.” Meanwhile, a competitor’s cap — built on 280 gsm pre-shrunk twill with a fused buckram backing — holds its silhouette through a season of wear. The raw material cost difference was about $0.30 per cap. The brand’s return rate on that SKU hit 14%.
Material selection isn’t just about weight. It’s about how the fabric behaves in the context of the cap’s construction method. A cap factory that understands this will ask about your climate target, your intended fit (low-profile vs. high-crown), and your decoration method before proposing a fabric. Here’s a quick reference we use internally:
|
Material |
Typical Weight (gsm) |
Breathability |
Shrinkage Risk (un-treated) |
Best Application |
|---|---|---|---|---|
|
Cotton twill |
250–280 |
High |
Moderate (5–8%) |
All-season structured caps |
|
Brushed cotton |
300–320 |
Medium |
Low (if pre-shrunk) |
Soft, unstructured dad hats |
|
Polyester mesh |
180–220 |
Very High |
None |
Athletic/trucker caps, hot climates |
|
Acrylic/Wool blend |
320–350 |
Low |
Low |
Cold-weather beanies, fitted caps |
A separate consideration: the sweatband. Most cap manufacturers default to a cotton/polyester blend. If your customer base is in the Gulf Coast — high humidity, 95°F summers — a moisture-wicking Coolmax sweatband reduces post-wash odor and customer complaints. The upgrade typically costs $0.08–$0.12 per unit. Worth it.
Mistake #3: Treating Communication as an Afterthought
Language barriers are the surface problem. The deeper problem is a factory’s internal communication structure. When you send a technical comment about embroidery digitizing, who sees it? In many large-scale cap factory operations, your email goes to a sales rep who forwards it to a merchandiser who translates it to a floor supervisor. If that chain breaks — and it does, often — you get a production sample that doesn’t match what you approved.
We’ve fixed this by collapsing communication to two touchpoints. The client speaks with a dedicated project manager who has direct access to the cutting and sewing floor, not just the sales desk. That person can send a photo of a stitching issue within 15 minutes of it happening, not 48 hours later when 2,000 pieces are already packed. Look for a cap manufacturer that can show you their escalation path, not just their quotation turnaround time.
A practical test: ask the factory to explain their process for handling an embroidery thread color mismatch spotted mid-production. If the answer is vague — “we will check and get back to you” — versus specific — “we stop that machine, pull the thread lot number, compare against the Pantone chip you approved, and re-thread within 20 minutes” — you’ve just learned more about their operation than any audit checklist will tell you.
Mistake #4: Skipping the Sampling Phase Because of Tight Deadlines
I’ve seen ecommerce brands push a cap factory to skip the pre-production sample because their launch date is locked and the factory lead time already consumed their buffer. They gamble. The factory ships the bulk order. Then the nightmare: the embroidery registration is off-center by 3mm, the sweatband tape is the wrong color, and the woven label is placed half an inch higher than approved. A 3mm shift on a six-panel cap puts the logo noticeably left of center in product photos. Customer trust evaporates.
Our QA team analyzed 2,200 orders from 2019 to 2023. Orders that bypassed the pre-production sample stage had a customer complaint rate 3.8 times higher than those that went through full sampling. Even when the bulk delivery happened on time, the cost of returns, reshipments, and the invisible cost of negative reviews erased the schedule gain.
A pre-production sample costs $120–$250 and takes 7–10 days. That’s the cheapest insurance you’ll ever buy. If the cap manufacturer resists — some do because sampling slows their line — negotiate a “sealed sample” approach: they produce two identical samples, sign both, keep one on file, and use the other as the production standard. No ambiguity.
Mistake #5: Assuming All Cap Factories Have the Same Quality Benchmarks
This is the gap that separates a cap factory that serves promotional distributors from one that serves high-end streetwear brands. Promo-grade caps prioritize speed and low cost; premium caps prioritize construction detail. Both are valid industries, but confusing one for the other leads to disaster. Here’s what the spec sheet typically doesn’t tell you:
|
Quality Parameter |
Promo-Grade Cap Factory |
Premium Custom Cap Manufacturer |
|---|---|---|
|
Embroidery stitch density |
6–8 stitches per linear inch |
10–12 stitches per linear inch |
|
Color fastness (AATCC wash test) |
Fades after 10–15 cycles |
Holds beyond 30 cycles |
|
Fabric shrinkage after 5 washes |
5–8% |
<2% (pre-shrunk and post-treated) |
|
Sweatband attachment |
Standard stitch, occasional puckering |
Dense zig-zag with minimal bulk |
|
Visor board consistency |
Varies, can soften after rain |
Consistent stiffness, waterproof-grade testing |
The irony is that the raw cost difference to move from “promo” to “premium” on these parameters is often less than $0.50 per unit. The real difference is process control. A cap factory that invests in tension-calibrated embroidery machines, climate-controlled fabric storage, and in-line QC checkpoints per 50 units will deliver that premium result without trying to upsell you. Ask for photos of their in-line QC station. If they can’t show you one, quality is being inspected only at the end — which means defects get packed and shipped.
New Generation’s production floor runs 12-point in-line checks per batch, and we track defect rates per operator daily. Over the past two years, that system has kept our external defect rate (found by client or third-party inspection) at 0.9% across 2.4 million units shipped. That’s not a brag — it’s a reference point you can use to calibrate other cap manufacturers you’re evaluating.
Mistake #6: Underestimating the Complexity of Custom Embroidery and Decoration
Embroidery is not a simple “upload logo and sew” process. The cap factory’s digitizer has to account for the curve of the cap, the fabric’s nap direction, and the underlying seams. A logo that looks crisp on a flat tee-shirt can pucker or distort when stitched across the center seam of a structured crown. We’ve re-digitized client artwork at least once, and often twice, to get the pull compensation and underlay stitching right.
A few practical parameters: on structured cotton caps, keep text no smaller than 0.2 inches in height to maintain readability. Stitch density above 10 SPI gives the cleanest edge, but the letters need an underlay stitch to prevent sink-in. 3D puff embroidery — popular for streetwear — requires a foam layer and double the normal stitch count; expect to pay about $0.85–$1.20 extra per location. Metallic and neochrome threads have lower tensile strength than standard rayon, so they break more often during high-speed runs. A skilled cap factory will slow the machine speed for those threads, which increases production time but avoids thread breaks that leave ugly loops on the crown.
If a cap factory accepts your logo file without questioning the stitch count, thread type, or digitizing approach, that’s a red flag. They’re treating it as a commodity job, not a custom build.
Mistake #7: Failing to Build a Long-Term Partnership With Your Cap Manufacturer
Transactional relationships create transactional results. When you hop from one cap factory to another chasing a $0.10 price cut, you reset the learning curve every time. A factory that knows your brand — your preferred sweatband tape, your typical embroidery issues, your seasonal peak periods — will pre-buy materials for you during raw material shortages, hold capacity during Q4 crunch, and call you before making a substitution that could surprise you.
This isn’t theoretical. During the 2021 polyester yarn shortage, some cap manufacturers quietly swapped 100% polyester for a poly-cotton blend on back panels without notifying clients — because those clients had no relationship equity. Factories prioritized their long-term partners for the remaining pure polyester stock. The brands that got burned were the ones who had never visited the factory floor, never had a video call with the production manager, and never placed more than two sequential orders.
Practical measures that deepen the partnership: commit to a quarterly forecast, even if it’s a range. Share your product roadmap so the cap factory can prepare new capabilities — maybe investing in a leather patch heat-press machine ahead of your fall collection. Pay on time. And visit the facility if you can. A single visit will teach you more about a cap manufacturer’s culture than 50 emails. The China-based factories that consistently serve U.S. brands well — including ours — rely on these long arcs of collaboration. It’s how we’ve kept some client relationships running for over a decade, through style shifts, tariff uncertainty, and a global pandemic.
The cap market will keep growing. PPAI data shows promotional headwear maintaining a steady 4–5% share of distributor revenue, and Statista’s projections for the baseball cap segment alone suggest compound annual growth exceeding 5% through 2028. The brands that win won’t be the ones who got the cheapest per-unit quote. They’ll be the ones who avoided these seven mistakes, built a spec-driven sourcing process, and locked in a cap manufacturer relationship that actually improves their product over time — not one that just ships boxes.
Baseball caps are not just a practical accessory for shielding your eyes from the sun or keeping your hair in place during outdoor activities. They have become a fashion statement, allowing individuals to showcase their personal style and creativity. In this article, we will explore the world of baseball cap design and how you can unleash your inner designer to create unique and customized caps that reflect your individuality.
Choosing a baseball cap manufacturer comes down to three verifiable things: dimensional tolerances held across a production run, consistency of finish on every unit, and packaging that protects and presents your brand on arrival. Use the TFP Gate — Tolerances, Finish, Packaging — to evaluate each candidate with documented evidence rather than claims. This guide gives you the questions, decision tables and checklists to do it.
Reviewing a first sample from a baseball cap manufacturer requires a structured framework rather than a visual glance. To compare suppliers objectively, use the 4-Pillar Sample Audit: assess Panel alignment, Pattern symmetry, Production consistency, and Print quality. Document every observation to ensure the final bulk order meets your private label's specifications.
To secure an accurate quote from a baseball cap manufacturer, you need a structured review pack: technical drawings, material specifications, commercial terms, and quality criteria. The Drawing-to-Delivery Review Framework helps procurement teams compare suppliers systematically, confirm capabilities, and document approvals before production begins.
Most rework in custom cap sourcing traces back to specification gaps: details left undefined in the quote and unconfirmed in writing before production. A baseball cap manufacturer can only build to what is documented. Buyers who apply a gate-based approval process — construction, materials, decoration, tolerances — catch gaps at the spec stage, when changes are cheap, instead of at inspection.
Evaluating a baseball cap manufacturer using only digital photographs creates severe sourcing blind spots. To compare samples effectively, you must implement a tactile evaluation framework that assesses material integrity, construction durability, and tolerance consistency through physical inspection and direct documentation.
Comparing two quotes from a baseball cap manufacturer means normalizing them onto identical line items — terms, add-ons, landed cost, compliance, verification and documentation — then scoring each gap. The supplier whose quote survives a line-by-line audit, not the lowest headline number, deserves your order.
A clean handoff from an approved sample to bulk production requires three things: a frozen physical reference both parties sign off on, a written specification that records every agreed attribute, and gate checkpoints that make production release conditional on documented verification. Choose a baseball cap manufacturer based on how well they support this process, not just on the sample itself.
When a revised sample from your baseball cap manufacturer still misses the mark, do not restart sourcing by reflex. Instead, run a structured comparison: tag each requested change, verify which were actually implemented, isolate the remaining defects by cause, and decide — with evidence — whether the gap is fixable within the current supplier relationship. Most revision problems are documentation problems in disguise, and a disciplined review loop resolves them faster than a factory switch.
A clear RFQ turns scattered buyer requirements into one comparable document every baseball cap manufacturer can answer the same way. Use the R-F-Q-3 framework: define Requirements precisely, fix the quote Format, request Qualifications evidence, and collect at least 3 responses. This article shows you how to build that document, score replies, and approve a supplier with documented confidence.